Imler
Imler
Explore our top-tier selection of intelligent commercial vending and self-service automated dispensing equipment built for high-traffic modern retail environments.
As global retail undergoes an accelerated transformation toward unmanned, automated commerce, sourcing from top-tier China snack dispenser manufacturers and automated retail factories has become a core strategic advantage for international brands. The modern automated food and snack dispensing industry transcends traditional mechanical vending. Today's ecosystem integrates IoT connectivity, high-precision robotic arms, intelligent payment gateways, and advanced thermal management to deliver a frictionless end-user experience while maximizing profitability per square foot for operators.
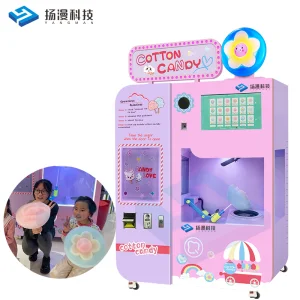
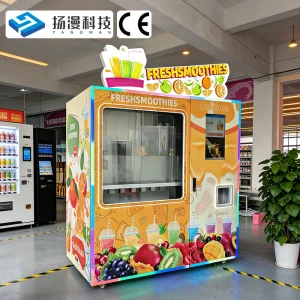
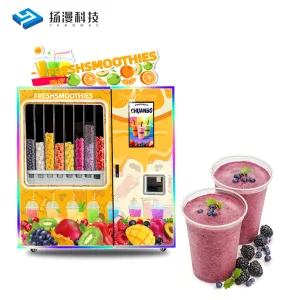
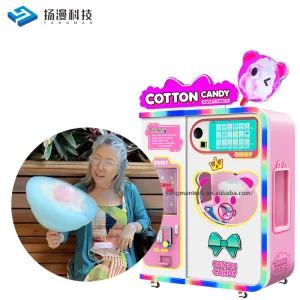
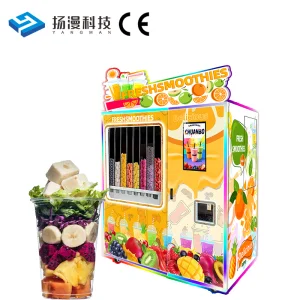
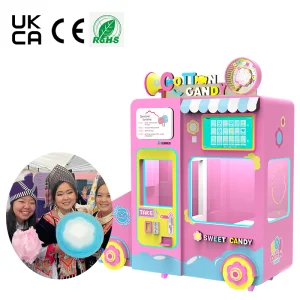
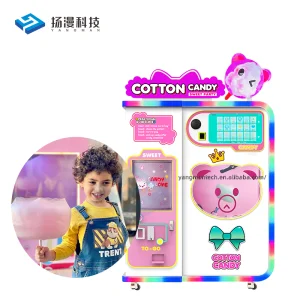
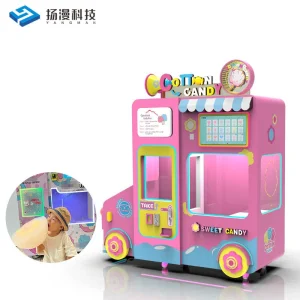
Global enterprises, retailers, and independent brand builders increasingly rely on Chinese manufacturing clusters due to their unmatched capacity for end-to-end customization, rapid prototyping cycles, and rigorous quality assurance frameworks. Whether deploying high-speed smoothie dispensers in transit hubs or interactive cotton candy and snack vending systems in amusement parks, partnering with an experienced Chinese factory ensures scalable growth, strict international compliance, and optimized supply chain resilience.
A transparent look at our production capacity, establishment background, and operational metrics.
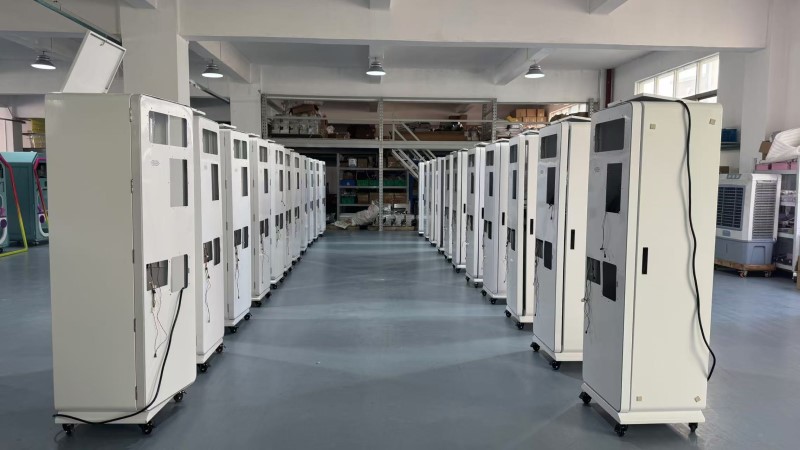
State-of-the-art assembly lines, rigorous quality control testing stations, and advanced R&D engineering laboratories.
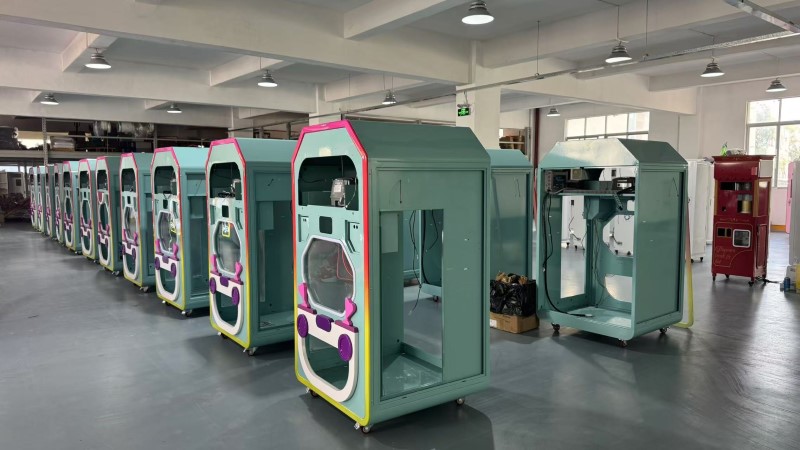
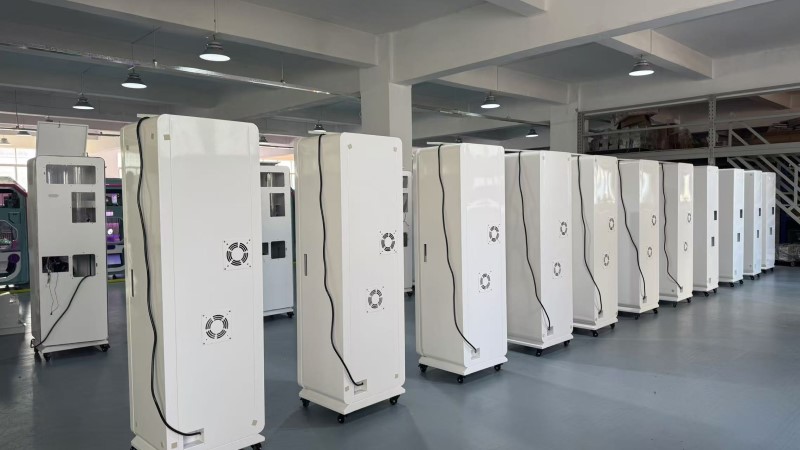
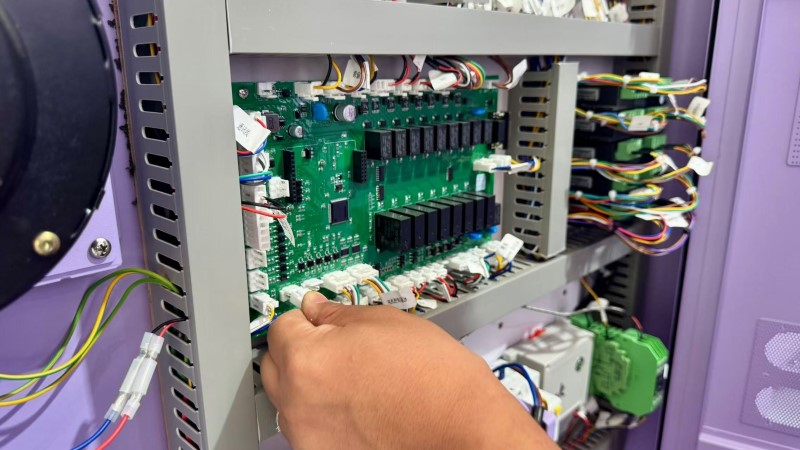
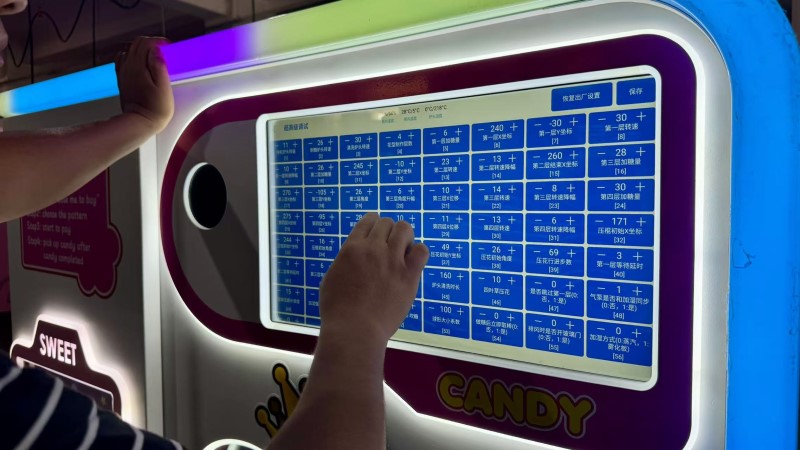
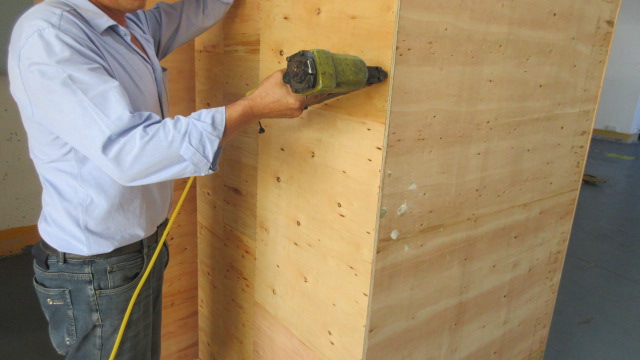
The evolution of snack dispensers and automated vending machines is being shaped by disruptive technologies including edge computing, AI-driven inventory prediction, and contact-less biometrics. Our R&D division is continuously pioneering intelligent dispensing architectures that feature real-time telemetry, remote firmware over-the-air (OTA) updates, and automated fault diagnostic reporting.
By integrating advanced ERP systems and automated sheet metal fabrication machinery across our 1,890-square-meter production floor, we achieve uncompromising manufacturing precision. Our supply chain resilience ensures stable component sourcing, short lead times, and flexible batch scaling for global B2B clients. From raw material input inspection to final burn-in stress testing, our rigorous QA protocol guarantees that every unit shipped meets international operational standards.
Exporting to over North America (25%), South America (16%), and Eastern Europe (15%) requires strict adherence to diverse regional electrical and safety mandates. Our product portfolio is fully backed by internationally recognized certifications, ensuring hassle-free customs clearance and safe deployment in public commercial venues worldwide.
Our products undergo rigorous testing by world-leading inspection agencies to ensure absolute safety, electrical reliability, and eco-friendliness.
 RoHS
TST20220780321-3RC
 UL
CU 72405025 0001
 KC
XU070727-23001A
 PSE
B-S2410C4262
 UKCA
CTICAF311241220042490DC
 CE
M.2022.206.C73909
UKCA
CTICAF311241220042489AC
PSE
PSE25072983
CE
CTICAF311241220042487DC
 CB
CN73011
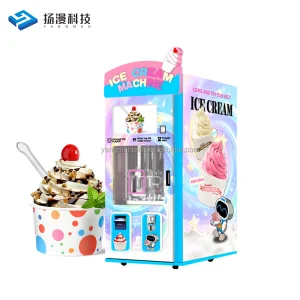
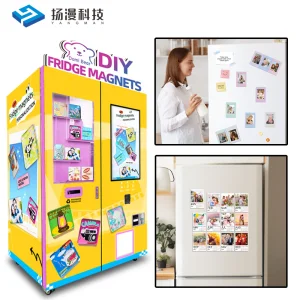
Discover our additional automated solutions tailored for diverse recreational venues, dessert shops, and customized printing retail.
Sourcing from top China manufacturers provides access to mature supply chains, advanced R&D capabilities, highly competitive production costs, and full custom OEM/ODM solutions tailored to international specifications.
Yes. Our product lineup complies with major global standards, holding certifications including CE, UL, RoHS, KC, PSE, UKCA, and CB, ensuring seamless regulatory compliance across North America, Europe, and Asia.
Depending on customization complexity and order volume, standard manufacturing and quality testing cycles range from 20 to 35 days, supported by our robust production capacity and efficient supply chain partners.